Factory-direct gas sensing instrumentation, smart controllers, and automated safety shut-off systems engineered for global supply chains.

Residential combustible gas alarm with dual acoustic-optic alert signals, low-drift micro-sensors, and solenoid linkage.
Trusted domestic gas safety device certified for high repeatability, fast response times, and zero false-alarm algorithms.
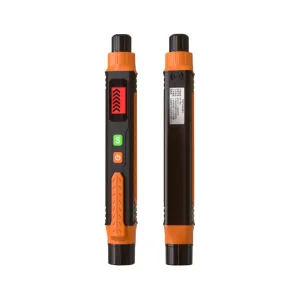
Ultra-compact pocket leak detection pen with high sensitivity for HVAC inspectors, pipeline crews, and meter auditing.

Explosion-proof point detector engineered with cast aluminum Ex d casing, 4-20mA/RS485 output for harsh process plants.

Streamlined residential natural gas and LPG alarm designed for volume OEM property development projects.
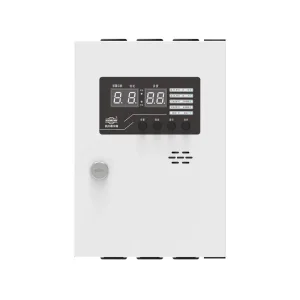
Multi-channel bus-system supervisory control panel supporting real-time data display, relay outputs, and event logging.

Industrial point-type detector with digital bus communication, local LED concentration screen, and non-intrusive IR calibration.

Rugged IP66 explosion-proof personal gas detector built for refinery spot-checks, utility vaults, and field service crews.
Engineering principles, optical cavity physics, and zero-drift algorithmic innovations driving modern Non-Dispersive Infrared (NDIR) gas detection systems.
Non-Dispersive Infrared sensing operates fundamentally on the Beer-Lambert Law, quantifying gas concentration ($C$) by measuring the attenuation of specific infrared light wavelengths as they traverse an optical absorption chamber of length ($L$):
Where I is the detected radiation intensity, I₀ is the initial emitter intensity, and α represents the target gas absorption coefficient. Sichuan Shield Technology integrates dual-beam optical configurations comprising an active measurement channel tuned to hydrocarbon resonance absorption (e.g., 3.31 μm for CH4 or 4.26 μm for CO2) alongside a non-absorbing reference channel (3.91 μm). This differential reference architecture dynamically eliminates optical drift caused by light source aging, mirror tarnish, and particulate accumulation.
To achieve exceptional thermal resistance, rapid transient response, and long operational lifetimes exceeding 10 years, our industrial OEM sensors utilize state-of-the-art MEMS (Micro-Electro-Mechanical Systems) infrared emitters paired with high-sensitivity pyroelectric or thermopile detectors.
| Performance Metric | Shield OEM NDIR Sensors | Catalytic Bead (Pellistor) | Electrochemical Sensors |
|---|---|---|---|
| Target Gas Spectrum | Combustible Hydrocarbons, Methane, CO2, Refrigerants | Combustible Gases ($0-100\%\text{ LEL}$) | Toxic Gases ($CO, H_2S, O_2, NH_3$) |
| Poisoning Susceptibility | Immune (Silicones, $H_2S$, Lead, Halogens) | High Risk (Permanently poisoned) | Moderate (Sensor degradation over time) |
| Oxygen Requirement | 0% Oxygen Needed (Works in Inert $N_2$ Gas) | Requires $>10\%\text{ }O_2$ to operate | Requires trace $O_2$ for chemical reaction |
| Operational Lifespan | > 10 Years (Light Source Limited) | 2 – 3 Years (Filament evaporation) | 1 – 2 Years (Electrolyte depletion) |
| Zero Calibration Stability | Self-correcting (Dual-Beam Auto Baseline) | High Drift (Requires quarterly recalibration) | Moderate Temperature Drift |
Deploying specialized NDIR infrared gas modules across hazardous process zones, smart city utility infrastructure, commercial HVAC, and green energy networks.
Refineries, offshore oil rigs, and chemical storage facilities present hazardous Zone 1 and Zone 2 environments where explosive hydrocarbon leaks ($C_1-C_6$) pose extreme risks. Shield's flameproof SIL2-certified NDIR transmitters provide continuous monitoring in oxygen-starved flare stack lines and inert purging environments where traditional catalytic sensors fail completely.
Municipal natural gas networks, underground valve chambers, and utility tunnels require battery-optimized low-power NDIR sensors capable of withstanding $100\%$ relative humidity and total water immersion. Integrated Modbus RS485 and IoT wireless modules enable remote telemetry monitoring across citywide gas distribution hubs.
From HVAC indoor air quality ($CO_2$ monitoring for demand-controlled ventilation) to next-generation low-GWP refrigerant leak detection ($R32, R1234yf, R290$), Shield supplies custom OEM sensor blocks engineered with precision temperature and humidity matrix algorithms to guarantee zero false tripping in commercial buildings.
Sichuan Shield Technology operates a state-of-the-art gas instrument manufacturing center in Chengdu, Sichuan—combining precision micro-assembly, automated calibration chambers, and stringent QA protocols.
As a recognized "Specialized, Refined, Distinctive and Innovative" High-Tech Enterprise holding over 40 technical patents, Shield eliminates intermediary trading markups by offering direct OEM sensor manufacturing. Our automated production line integrates high-speed SMT surface mounting, robotic laser optical alignment, and hermetic sealing for explosion-proof housings.
Every infrared module undergoes rigorous environmental stress screening (ESS), cycling across full industrial temperature profiles from -40°C to +75°C inside automated gas calibration matrices. Multi-point temperature compensation coefficients are embedded directly into on-board flash microcontrollers prior to shipment.
Flexible hardware pinouts, communication protocols, custom optical path lengths, and co-developed firmware tailored for international instrument manufacturers.
Seamlessly adapt our sensor engines into your instrument motherboard. Supported digital and analog interfaces include UART TTL, Modbus-RTU RS485, 4-20mA industrial current loops, and voltage outputs ($0.4V - 2.0V$), with custom pinout geometries matching industry standard footprints.
From trace-level CO2 ($0-2000\text{ ppm}$) for IAQ applications up to high-concentration Methane ($0-100\%\text{ Vol}$) for biogas digesters, our optical engineers adjust cavity path lengths ($10\text{ mm}$ to $300\text{ mm}$) and select specific infrared filters to match your target detection range.
We provide full OEM turnkey branding, laser-etched stainless steel labeling, custom packaging, software user interface modification, and comprehensive test documentation required for rapid ATEX, IECEx, UL, and CE regional certification.
Ensuring seamless deployment across European, North American, Asia-Pacific, and Middle Eastern regulatory environments.
Navigating international gas safety directives requires strict adherence to electro-technical and explosion protection standardizations. Shield OEM sensor modules and complete detector systems are engineered to conform with:
Global engineering procurement demands rapid technical consultation across time zones. Our bilingual application engineering department delivers dedicated OEM customer support:
Complete the safety protection loop with high-reliability aluminum shut-off valves, specialized household detectors, and commercial point monitors.

Precision aluminum alloy pulse solenoid shut-off valve designed for instant pipeline isolation upon detector alert signal.
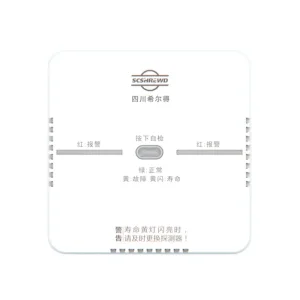
Modern aesthetic residential gas leak monitor featuring automated self-diagnostics and direct solenoid driver relay.
High-precision methane and LPG kitchen gas detector certified for residential apartments and urban housing projects.
Heavy-duty industrial gas transmitter providing continuous concentration feedback for factory supervisory systems.
Fully customizable OEM domestic gas safety solution packaged for international gas utilities and appliance brand owners.
Reliable gas leak detection device built with high stability micro-sensing element for long-term residential safety.
Ultra-reliable compact gas detector engineered for easy wall mounting, fast plug-and-play setup, and valve linkage output.

Stand-alone commercial gas detector with built-in high-decibel siren, warning beacon, and local alarm status output.
Expert technical answers to key questions asked by instrument designers, procurement directors, and system integrators.
