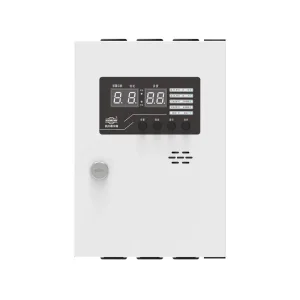
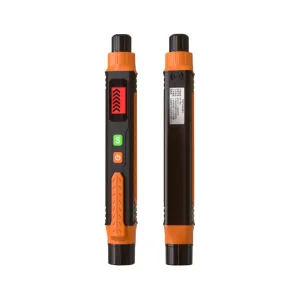
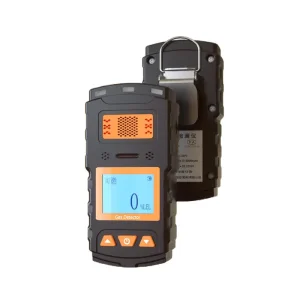
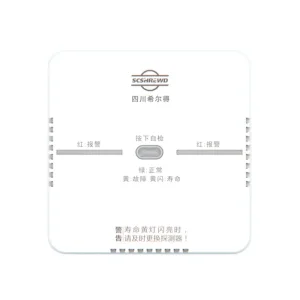
Factory-direct hardware portfolio covering industrial fixed transmitters, portable multi-gas monitors, emergency solenoid valves, and central alarm management panels.
Modern industrial automation, intelligent building engineering, and carbon footprint compliance frameworks have driven a monumental shift in ambient gas detection requirements. Beyond traditional Lower Explosive Limit (%LEL) monitoring for combustible hydrocarbon threats, procurement engineers and system integrators now require high-precision Carbon Dioxide (CO2) PPM (Parts Per Million) detectors capable of sub-ppm sensitivity, minimal baseline drift, and seamless edge-computing integration.
Carbon dioxide is both a vital process indicator and a lethal workplace hazard. In indoor air quality (IAQ) systems, CO2 accumulation directly impacts cognitive performance and ventilation efficiency. In industrial refrigeration (R744 / CO2 systems), agricultural greenhouses, carbon capture and storage (CCS) hubs, and underground utility vaults, undetected CO2 displacement poses severe hypercapnia and asphyxiation risks. Consequently, sourcing an authoritative OEM CO2 PPM detector supplier and factory capable of delivering hardware-level durability, custom optical architecture, and verified factory calibration is paramount for global B2B buyers.
To establish absolute technical clarity for procurement engineers, gas detection methodologies for Carbon Dioxide cannot rely on standard catalytic bead or electrochemical sensors due to the inert chemical structure of CO2. Gas detection factories deploy specialized Non-Dispersive Infrared (NDIR) spectroscopic techniques alongside photoacoustic sensing platforms.
| Sensing Architecture | Target Dynamic Range | Interference Susceptibility | Operational Lifespan | Recommended OEM Application |
|---|---|---|---|---|
| Dual-Beam NDIR Spectroscopy | 0 – 5,000 ppm / 0 – 5.0% VOL | Immune to humidity, poisonous gases & O2 displacement | 10 – 15 Years | Industrial Process Safety, Refrigeration Leakage, OEM IAQ Transmitters |
| Single-Beam NDIR with ABC | 400 – 2,000 ppm | Slight baseline drift under continuous 24/7 high-CO2 occupancy | 5 – 8 Years | Standard Commercial HVAC & Smart Building Automation |
| Photoacoustic Spectroscopy (PAS) | 0 – 10,000 ppm | Vulnerable to extreme acoustic vibration and micro-shocks | 5 – 10 Years | Ultra-compact wearable devices, smart home consumer electronics |
| Solid-State Electrochemical (Trace) | 0 – 1,000 ppm | Cross-sensitive to VOCs, humidity fluctuations, acidic gases | 2 – 3 Years | Legacy low-cost ambient indicator units (Not recommended for safety) |
Our OEM carbon dioxide sensing chambers incorporate precision-machined gold-plated optical wave-guides operating at a narrow absorption band of 4.26 μm. At this exact wavelength, CO2 molecules exhibit peak infrared energy absorption without interference from ambient water vapor (H2O) or methane (CH4). By integrating an internal reference detector operating at 3.91 μm, Sichuan Shield Technology’s OEM modules continuously measure optical intensity changes, compensating automatically for lamp aging, dust accumulation, and temperature gradients.
A stand-alone OEM CO2 detector is only as effective as its surrounding control architecture. As a primary manufacturer based in Chengdu, China, Shield provides complete end-to-end integration across five critical macro-industrial sectors:
Transcritical CO2 refrigeration systems operate under severe high pressures exceeding 100 bar. Small seal failures cause massive CO2 gas dumps. Shield fixed gas detectors interface directly with industrial pulse solenoid shut-off valves (e.g., JYFJS-011 series) to automatically isolate high-pressure liquid lines upon detecting >5,000 ppm leaks.
Compliant with ASHRAE 62.1 and RESET Air standards, our custom OEM indoor air quality detectors output Modbus RTU / RS485 and 0-10V analog signals. Automated Demand-Controlled Ventilation (DCV) lowers energy consumption by activating fresh air dampers only when human respiration pushes indoor CO2 past 800–1,000 ppm thresholds.
Commercial agricultural facilities boost crop yields through controlled carbon dioxide enrichment up to 1,200 ppm. Shield OEM sensing modules provide relay contact outputs to precisely meter CO2 injection valves while ensuring worker safety cutoff alarms at 5,000 ppm (OSHA PEL limit).
Maintenance personnel entering breweries, beverage bottling plants, or municipal vaults face acute asphyxiation hazards. Our ruggedized, portable multi-gas monitors (e.g., BTYQ-Z4 and JLY-CP100 series) feature micro-pump sampling and triple alarms (audible, visual, haptic) engineered for hazardous zones.
Early-stage thermal runaway in lithium-ion battery banks releases off-gas containing off-target trace gases and CO2 spikes prior to visible smoke or open flames. Shield point-type transmitters linked to central alarm controllers give facility operators critical early-warning intervention windows.
Pairing point-type transmitters with instant electromagnetic shut-off valves ensures complete physical hazard isolation. Our JYFJS-011 valves feature an aluminum alloy body design engineered for zero leakage, requiring manual reset after an alarm event to mandate human site verification before gas line re-pressurization.
Exporting gas detection equipment across North America, Europe, the Middle East, and Southeast Asia requires rigorous adherence to regional regulatory directives. Sichuan Shield Technology operates under fully audited quality control processes to simplify global market entry for OEM partners.
Industrial installations in classified hazardous locations mandate explosion-proof enclosure verification. Shield fixed transmitters are engineered to meet strict Ex d IIC T6 Gb explosion-proof enclosures, alongside mandatory China 3C certification, CE electromagnetic compatibility (EMC), and RoHS/REACH environmental compliance.
For high-risk industrial safety loops (Functional Safety according to IEC 61508 / IEC 61511), gas safety systems require certified hardware fault tolerance. Our gas alarm controllers and fixed detectors incorporate internal self-diagnostic routines, supervising sensor element integrity, relay line continuity, and internal power supply voltages 24/7.
Located in the Southwest Airport Economic Development Zone in Chengdu, Sichuan Shield Technology Co., Ltd. operates a high-tech manufacturing center integrating modern Surface Mount Technology (SMT) lines, automated optical inspection (AOI), and environmental testing chambers.
High-speed Surface Mount lines ensure precision micro-soldering for NDIR signal processing circuitry.
Every OEM detector passes through automated calibration manifolds utilizing certified standard span gas mixtures.
100% of sensor modules undergo high/low temperature environmental stress screening before shipment.
Over 40 granted patents covering gas detection algorithms, optics, and emergency shut-off valve mechanics.
We streamline the custom design process for overseas brand owners, engineering procurement contractors (EPCs), and industrial system distributors. Our engineering support structure ensures transparent product lifecycle delivery:
Define target gas species (CO2, CH4, LPG, CO, O2, H2S), detection scales (PPM vs %LEL vs %VOL), custom Modbus registry maps, alarm threshold logic, and relay activation patterns.
Custom silkscreen logo printing, private label front panel overlay design, customized enclosure colorways, and bespoke PCB layout adaptations for existing customer housings.
Fully automated assembly, batch calibration reports, export packaging, compliance documentation clearance, and flexible shipping arrangements (FOB, CIF, DDP, EXW).
Expert responses to critical engineering and purchasing inquiries regarding CO2 PPM detection, sensor mechanics, and supplier selection.
Explore our full suite of certified gas control accessories, point-type alarms, and emergency shut-off valves direct from our Chengdu factory.
Looking for custom OEM CO2 PPM detectors, point-type flammable gas alarms, or high-reliability emergency shut-off valves? Connect directly with our engineering sales director today.