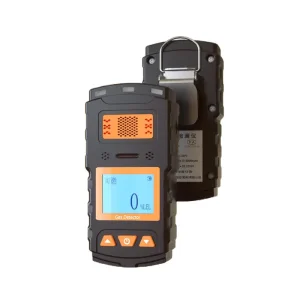
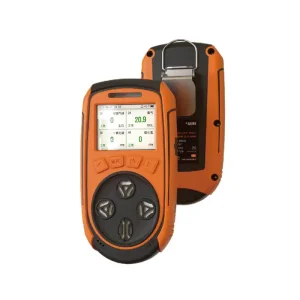
Explore our top-tier OEM/ODM gas detection hardware, point-type sensors, and solenoid emergency shut-off valves engineered for direct power integration, zero-latency response, and seamless SCADA/BMS connectivity.
Why hardwired CO detection remains the gold standard for high-occupancy commercial developments, boiler rooms, industrial process facilities, and municipal utility networks.
Carbon monoxide (CO) is a color-free, odorless, and tasteless toxic gas generated by the incomplete combustion of carbon-containing fuels. In industrial process plants, commercial boiler facilities, enclosed parking structures, and residential multi-family complexes, a failure in CO monitoring can lead to catastrophic life-safety hazards within minutes.
While standalone battery-powered CO alarms serve basic residential retrofits, industrial-grade protection demands hardwired CO detector architecture. Operating on continuous 110V/220V AC line power or standardized 24V DC industrial power loops (such as 4-20mA or RS485 Modbus-RTU), hardwired units eliminate the risk of dead batteries, signal attenuation, or maintenance oversights. More importantly, hardwired systems enable direct dry-contact output linkage to automated solenoid valves (e.g., JYFJS-011 series), exhaust ventilation fans, and centralized Building Management Systems (BMS).
Hardwired systems ensure zero-latency relay actuation (<1 second) to trigger emergency shut-off valves and HVAC fresh-air purge systems long before toxic concentrations reach dangerous thresholds.
Macro-economic shifts, regulatory mandates, and smart building integration are altering how international buyers procure hardwired gas safety hardware.
Global building codes (such as EN 50291, UL 2034, NFPA 720, and China’s mandatory GB 15322 standard) increasingly require hardwired CO detectors with mandatory backup batteries and physical linkage outputs in commercial catering, hotels, residential developments, and public spaces.
Modern facility operators reject isolated alarms. Procurement is shifting toward hardwired CO detectors equipped with RS485 Modbus-RTU, BACnet, or 4-20mA analog interfaces, allowing continuous real-time PPM data logging, remote zero-drift diagnostics, and automated cloud alerting.
As commercial heating transitions to hydrogen-blended natural gas and high-efficiency boilers, background gas compositions change. Factory suppliers must engineer advanced electrochemical sensors with integrated H2-elimination filters to eliminate cross-sensitivity false alarms.
A comprehensive comparison for system integrators, EPC contractors, and OEM buyers evaluating hardware topologies for critical installations.
| Performance / Spec Metric | Hardwired Industrial CO System | Hardwired Bus-Type (RS485) | Standalone Battery CO Alarm |
|---|---|---|---|
| Primary Power Supply | 110V/220V AC Line Power / 24V DC Loop | 24V DC 4-Wire Bus (Power + Data) | Internal Lithium/Alkaline Battery |
| Linkage & Shut-off Control | Direct Relay (Solenoid Valve / Exhaust Fan) | Central Controller Automated Trip | Audible Buzzer Only (No Linkage) |
| Response Latency (T90) | < 30 Seconds (Real-Time Sensing) | < 15 Seconds (Polled High-Speed) | Variable (Duty-Cycle Pulsed) |
| Sensor Technology | Industrial Micro-Electrochemical / NDIR | Temperature-Compensated Electrochemical | Basic Commercial Electrochemical |
| Enclosure Protection | IP65 to IP67 Cast Aluminum / PC Plastic | IP66 Flameproof / Explosion-Proof | IP20 Light Residential ABS |
| Central System Integration | 4-20mA Analog / Dry Contacts | RS485 Modbus-RTU / BACnet IP | None (Isolated Local Unit) |
| Design Service Life | 5 to 10 Years (Replaceable Sensor Module) | 8 to 10 Years Continuous | 2 to 3 Years Max |
Tailored architecture designs for commercial HVAC, municipal utilities, petrochemical process units, and large residential real estate projects.
Commercial gas boilers pose simultaneous risks of combustible gas leaks (CH4/LPG) and incomplete combustion toxic hazards (CO). Our macro solution pairs hardwired point-type CO detectors (SD2100A series) and combustible detectors with centralized controllers (SD8001 series) linked directly to high-pressure aluminum alloy electromagnetic shut-off valves (JYFJS-011). In the event of a breach, gas supply is isolated at the header pipe instantly.
Vehicle exhaust accumulation in enclosed parking garages demands continuous multi-zone CO monitoring. Hardwired RS485 bus-type detectors (SD2100E series) monitor ambient CO concentration continuously. When levels cross preset limits (e.g., 35 PPM or 50 PPM), the system automatically spins up jet ventilation fans to purge the area, balancing indoor air quality (IAQ) and energy consumption.
In steelworks, chemical synthesis units, and gas storage depots, extreme ambient temperature variations, chemical vapors, and dust are common. Industrial-grade explosion-proof point detectors equipped with cast-aluminum flameproof enclosures and anti-poisoning electrochemical sensors provide SIL-2 certified continuous surveillance, interfaced directly into plant SCADA systems via 4-20mA loops.
As a direct high-tech factory in Chengdu, China, Sichuan Shield Technology delivers end-to-end engineering, manufacturing, calibration, and international certification support for enterprise buyers.
Every hardwired CO detector and automated valve leaving our production line undergoes stringently audited quality checks:
We partner with regional safety brands, gas utilities, and system integrators to manufacture tailored safety equipment:
Navigating complex international safety standards requires robust documentation, certified quality systems, and structured lifecycle support.
Our products hold China’s mandatory 3C certification, ISO 9001 quality management standards, and over 40 technical patents. For export projects into Europe, the Middle East, Southeast Asia, and the Americas, our engineering team works directly with buyers to provide sample test dossiers, EN 50291/UL 2034 compliance testing, and CE certificate validation.
Hardwired CO detectors require periodic bump testing and calibration (typically every 12 to 24 months depending on environmental severity). We supply factory-calibrated replacement sensor pods, portable span gas calibration kits, and detailed video calibration guides, ensuring facility maintenance engineers maintain peak system accuracy.
From initial project wiring schematic reviews to post-sale technical trouble-shooting, our English-speaking technical sales engineers provide direct support. Importers and EPC contractors receive tailored technical proposals, bulk volume tiered pricing, and guaranteed production lead-times.
How next-generation sensor technology, machine learning drift compensation, and ultra-low power buses are transforming hardwired carbon monoxide safety.
Transitioning from analog raw output sensors to onboard ASIC digital sensor modules that continually monitor electrolyte hydration levels, electrode impedance, and temperature/humidity compensation, reducing false positives caused by sudden ambient shifts.
Embedding lightweight machine learning algorithms directly into hardwired gas alarm controllers. By evaluating gas rise rates and spatial diffusion curves, the system distinguishes between benign transient background spikes (e.g., momentary diesel generator start-up exhaust) and genuine hazardous leaks.
Pioneering non-consumable NDIR and MEMS solid-state carbon monoxide sensing technologies for hardwired industrial units. Eliminating chemical degradation enables a decade of continuous service with zero sensor element replacement requirements.
Complete your safety system specification with our expanded range of commercial gas detectors, multi-gas portable analyzers, and high-reliability safety shut-off hardware.
Direct technical answers from our engineering team covering hardwired installation, valve linkage wiring, sensor cross-sensitivity, and factory procurement.