Explore our high-reliability, hardwired monitoring detectors, industrial controllers, and automatic gas safety valves deployed worldwide.
In modern industrial, commercial, and residential infrastructure, fire detection systems are no longer standalone smoke alarms. Modern life-safety design demands comprehensive integrated environments capable of identifying thermal anomalies, toxic combustion byproducts, and explosive gas leaks simultaneously. As a specialized wholesale mains powered fire detection system supplier and manufacturer, our technical framework prioritizes uninterrupted operational continuity via hardwired AC power mains (110V–240V 50/60Hz) coupled with rechargeable sealed secondary lithium or Ni-MH battery reserves.
Unlike purely battery-powered wireless consumer alarms that are vulnerable to signal attenuation, battery depletion, and high maintenance overhead in large facility footprints, mains powered fire detection systems deliver continuous high-current power required for multi-sensor arrays, high-decibel piezo sounders, relay linkage drives, and real-time IoT bus communications. This engineering whitepaper outlines the global procurement trends, technical architectures, compliance frameworks, and system integration strategies for B2B buyers, system integrators, EPC (Engineering, Procurement, and Construction) contractors, and municipal gas utility authorities.
Understanding the engineering demands of commercial property developers, industrial plant operators, and municipal safety buyers.
Commercial and multi-family projects mandate 230V/110V AC direct wiring with fail-safe zero-downtime battery backup (recharging automatically), compliant with international building codes (e.g., BS 5839-6 Grade D1/C, NFPA 72).
Global procurement teams favor detection systems that go beyond passive alarming by featuring dry-contact relay linkage outputs to automatically actuate pulse solenoid emergency shut-off valves, exhaust ventilation, and HVAC damper isolation.
Modern tenders demand multi-gas and combustion smoke synergy. Systems must combine photoelectric chamber optics for smoldering fire with catalytic bead or NDIR (Non-Dispersive Infrared) sensors for CH4/LPG gas detection.
Distributors require tailored enclosure designs, private labeling, localized alarm set-points (e.g., 7% LEL vs 10% LEL), custom wire terminal blocks, and custom packing documentation to streamline market-specific entry.
Inside the dual-processor circuitry, signal conditioning, and false-alarm suppression algorithms of Shield detection systems.
Mains powered fire and gas detection units operate in complex EMC (Electromagnetic Compatibility) environments subject to voltage surges, radio frequency interference (RFI), and ambient temperature fluctuations. Our factory engineers employ a multi-stage power conditioning module converting 85V–265V wide-voltage AC input into stabilized 12V/5V DC rails, equipped with varistor transient voltage suppression (TVS) rated to IEC 61000-4-5 standards.
| System Component | Technical Specification | Engineering Benefit |
|---|---|---|
| Primary Power Supply | AC 110V – 240V 50/60Hz Wide Range | Universal grid compatibility; immune to regional brownouts. |
| Secondary Power Backup | Rechargeable Ni-MH / LiFePO4 Cell (800mAh–2000mAh) | Provides 24+ hours of continuous monitoring during power outages. |
| Detection Technologies | Dual Infrared + Catalytic Bead + Photoelectric Optical | Eliminates cross-sensitivity to cooking fumes, humidity, and dust. |
| Output Linkage Signal | Pulse Voltage Output (DC 9V–12V) & SPDT Relay Contact | Directly drives solenoid valves (e.g., JYFJS-011) and fan relays. |
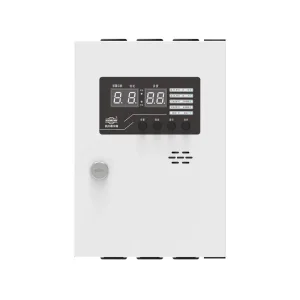
| Bus Communication | RS-485 Modbus RTU / M-Bus / 4-20mA Analog | Seamless integration with centralized SD8001 series alarm controllers. |
| Alarm Decibel Level | ≥ 85dB at 3 Meters (Piezoelectric Buzzer) | Guarantees audibility across loud commercial and industrial zones. |
| Enclosure Material | Flame-Retardant ABS + PC (UL 94 V-0 Rated) | High impact resistance, anti-static, self-extinguishing housing. |
Tailored protection topologies designed for specific hazard profiles and infrastructure scale.
Hazard Profile: Methane/LPG pipeline leaks, smoldering electrical fires, kitchen accidents.
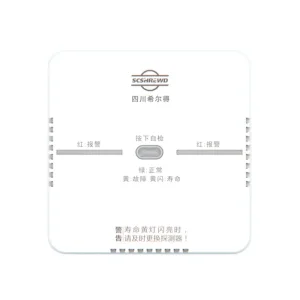
System Configuration: Mains powered SD6200 / SD6101 series hardwired detectors interconnected across rooms. Linked to a fast-acting electromagnetic solenoid shut-off valve installed at the main gas meter entry point.
Hazard Profile: High gas volume consumption, boiler burner flameout, CO toxic build-up.
System Configuration: Wall-mounted GTY-SD2130 point-type detectors connected via RS485 bus to a central Shield 8001AB control panel in the security office, automatically initiating ventilation blowers upon Low-Alarm trigger.
Hazard Profile: Explosive atmospheres (Zone 1 / Zone 2), toxic gas release, dust hazards.
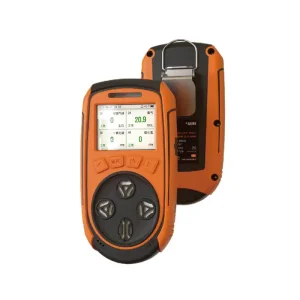
System Configuration: Heavy-duty explosion-proof point-type detectors (SD2100E Series) in cast-aluminum alloy housings, certified for harsh environmental duty with IR remote calibration.
Pioneering smart gas and fire safety through AI edge analytics, wireless mesh networks, and IoT cloud platforms.
Integration of low-power MCU chips executing real-time machine learning algorithms directly on the mains-powered detector board. Automatically filters out transient environmental spikes, humidity changes, and cooking oil vapours to guarantee zero false alarms.
Combining the reliability of 230V AC continuous power with wireless NB-IoT/Matter telemetry. Detectors self-organize into dynamic mesh networks, transmitting real-time sensor health, degradation telemetry, and concentration maps directly to municipal smart city dashboards.
Transition toward lifetime solid-state optical gas sensors requiring zero field calibration over a 10-year lifespan. Autonomous emergency isolation systems featuring integrated predictive AI to shut down gas lines *before* LEL thresholds are breached.
Why leading safety equipment distributors and EPC brands choose Sichuan Shield Technology as their direct factory partner.
Headquartered in the high-tech industrial manufacturing hub of Chengdu, China, Sichuan Shield Technology Co., Ltd. is a certified High-Tech Enterprise and a specialized manufacturer integrating R&D, SMT assembly, testing, and international logistics. Spanning more than 18 years of technical accumulation, our factory operates standardized automated production lines capable of producing over 80 marketable safety models.
Every mains-powered unit undergoes rigorous gas concentration chamber testing using certified standard reference gases, ensuring precision response times (T90 < 30s) prior to shipment.
From PCB layout modification and enclosure tooling to localized user interface design, we provide complete turnkey manufacturing solutions for global brand partners.
Backed by China Compulsory Certification (3C), ISO 9001 quality management, and over 40 technical patents, ensuring full compliance for international export.
Combine mains-powered detectors with high-integrity shut-off valves and multi-channel alarm controllers.
Engineered solutions to common procurement, wiring, standards, and system design queries.