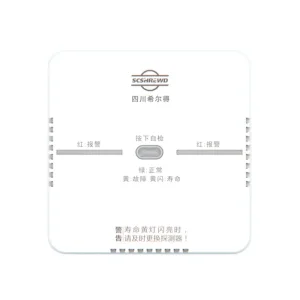
Standard-compliant, precision-calibrated detectors and electromagnetic isolation valves engineered for high-volume wholesale distribution and municipal engineering.




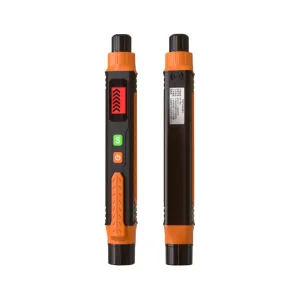
Analyzing macro-economic forces, regulatory shifts, and technical specifications driving bulk procurement across international gas utilities, real estate developers, and safety distributors.
Property developers and multi-family housing groups require compact, aesthetically modern household combustible gas detectors (such as the SD6101 and SD6103K series). Key procurement vectors prioritize zero false alarms, long operational lifespan (>5 years), low power consumption, and seamless interoperability with smart home hubs via Zigbee, Matter, or Tuya wireless protocols.
Natural gas utilities supplying Methane ($CH_4$) and Liquefied Petroleum Gas (LPG/Propane/Butane) focus on strict failure rate thresholds and system longevity. Procurement criteria dictate mandatory automated solenoid valve linkage (e.g., JYFJS-011 aluminum alloy series), ensuring that when gas concentrations reach 7% to 10% LEL, physical isolation occurs instantly without human intervention.
Commercial kitchens, hotel dining rooms, and district heating boiler facilities present high-risk environments with continuous heat, airborne grease, and humidity. Buyers in this segment demand heavy-duty point-type detectors (SD2130, SD2100E) housing poison-resistant catalytic sensors, IP65/IP66 enclosure protection, and RS485 Modbus RTU communication to centralized alarm panels (SD8001 series).
A comparative analysis of gas detection sensing mechanisms, false alarm mitigation algorithms, and micro-electronic circuit design.
| Sensor Technology Type | Primary Target Gases | Typical Sensitivity Range | Target Lifespan | Poisoning Susceptibility | Recommended Application |
|---|---|---|---|---|---|
| Planar Semiconductor (MOS) | Methane ($CH_4$), LPG, Iso-butane | 3% LEL – 20% LEL | 5 to 7 Years | Moderate (High Silicone sensitivity) | Standard Domestic Gas Alarms (SD6101/SD6200) |
| Catalytic Bead (Pellistor) | Combustible Gases ($CH_4$, $C_3H_8$, $H_2$) | 0% LEL – 100% LEL | 3 to 5 Years | High (Vulnerable to $H_2S$, Siloxanes) | Commercial Point Detectors (SD2100A / SD2130) |
| Non-Dispersive Infrared (NDIR) | Hydrocarbons, $CO_2$, $CH_4$ | 0% LEL – 100% Vol | 10+ Years | Immune to chemical poisoning | High-End Industrial & Explosive Zones |
| Electrochemical Cell | Carbon Monoxide ($CO$), $H_2S$, $O_2$ | 0 – 1000 PPM | 2 to 5 Years | Low (Vulnerable to solvent drying) | Dual Gas (Combustible + CO) Alarms & Portables |
How Shield unifies field detectors, central supervisory controllers, and pulse-driven solenoid valves into a zero-latency safety web.
Wall-mounted or ceiling-mounted residential detectors continuously sample room atmosphere via natural diffusion. Upon reaching 7% LEL, the detector initiates visual LED flashing and a local 85dB piezo-buzzer alert, notifying occupants of early gas accumulation before ignitable concentrations form.
If concentrations escalate past 10% – 15% LEL, the internal MCU trips the onboard relay, simultaneously transmitting a 12V DC electrical pulse (50ms duration) down the signal line while broadcasting cloud alerts via NB-IoT or Wi-Fi to property management dashboards.
The electric pulse triggers the JYFJS-011 Electromagnetic Valve. Utilizing a permanent magnet latch mechanism, the valve disc drops within <0.5 seconds, severing the gas supply at the main meter manifold. Crucially, the valve remains mechanically locked open/closed, requiring manual intervention to reset after safety verification.
In commercial complexes or multi-story buildings, point-type industrial detectors (SD2100E/SD2130) communicate over an RS485 M-Bus loop with central panels (SD8001A/B). Facility engineers monitor real-time gas concentrations, sensor drift logs, line fault status, and valve positions across thousands of nodes.
Engineered to conform with rigorous international life-safety mandates, metrology certifications, and automated manufacturing QA systems.
Navigating global market access requires strict adherence to localized safety certifications. Sichuan Shield Technology products are tested and validated to comply with key international directives:
Operating from our high-tech manufacturing park in Chengdu, China, Shield operates automated production lines featuring multi-stage gas calibration chambers. Every single detector undergoes a standardized quality loop:
Tailored manufacturing solutions empowering global brands, regional distributors, and gas engineering firms.
Custom enclosure molds, colorways, corporate logo silk-screening, and specialized mounting brackets designed to complement high-end residential interiors or rugged industrial sites.
Customization of communication stacks (Modbus RTU, BACnet, MQTT, Zigbee, NB-IoT, Matter), custom alarm setpoints, language localization for manuals, and customized voice-prompt audio chips.
Full engineering backing for regional market entry, including provision of schematic diagrams, PCB layout files, test reports, and factory sample units for local laboratory testing (CE, FCC, UL, local metrology approvals).
Engineering and procurement insights addressing technical specifications, installation best practices, and order fulfillment.
Explore additional factory-direct products engineered for wholesale supply and commercial deployments.