Factory-direct OEM/ODM portable gas leak detectors, 4-in-1 safety monitors, and point-type gas transmitters for enterprise safety deployment.

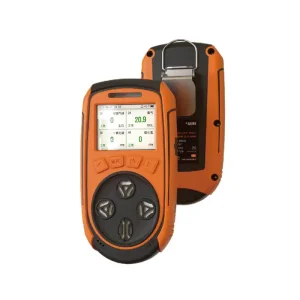

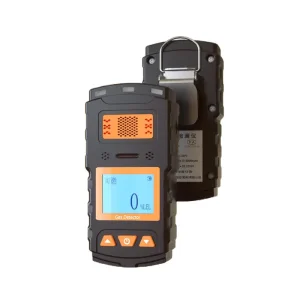



Why Tier-1 industrial enterprises, EPC contractors, and OEM distributors prioritize long-term stability and sensor cross-sensitivity suppression in Sulfur Dioxide detection.
Sulfur Dioxide (SO2) is a toxic, corrosive gas governed by strict OSHA, NIOSH, and EU-OSHA occupational exposure limits (TWA 2 ppm, STEL 5 ppm). Global industrial plants require continuous ambient monitoring to prevent respiratory poisoning and infrastructure corrosion.
In coal-fired power plants, copper/zinc smelters, and sulfuric acid manufacturing plants, SO2 concentration must be measured continuously in raw gas lines and post-scrubber exhaust stacks to optimize limestone dosing and ensure zero regulatory penalties.
Modern B2B buyers demand SO2 meters equipped with MODBUS RS485, 4-20mA analog signals, HART protocols, and wireless LoRaWAN modules to communicate directly with DCS/PLC networks and centralized safety supervision panels.
Standard electrochemical SO2 sensors often exhibit strong cross-sensitivity to Hydrogen Sulfide (H2S), Nitrogen Dioxide (NO2), and Carbon Monoxide (CO). Shield Technology's OEM factory integrates dual-channel differential electrochemical cells with internal catalytic filters, reducing cross-talk error to <2% F.S. in complex chemical gas matrix environments.
Tailored gas detection architecture for high-risk industrial facilities, processing plants, and municipal infrastructure.
Continuous fixed-point monitoring around coal burners, flue scrubbers, and stack emissions. Fixed SO2 transmitters linked to high-decibel audible-visual alarms and automated damper controls keep ambient levels safe for utility staff.
In sulfur recovery units (SRU) and hydrotreating facilities, fugitive SO2 emissions pose instant health risks. Our explosion-proof (Ex d IIC T6) SO2 transmitters provide reliable 24/7 supervision under extreme temperatures (-40°C to +70°C).
SO2 is widely used as a preservative and anti-microbial agent in winemaking and dried fruit processing. OEM portable SO2 meters safeguard personnel entering fermentation cellars, storage tanks, and barrel rooms during dosage operations.
Bleaching processes utilize sulfur compounds that emit hazardous SO2 vapors. Integrated gas safety chains—combining point-type SO2 sensors, central alarm controllers, and automatic electromagnetic solenoid shut-off valves—instantly isolate gas lines during leak events.
Comparing core detection technologies and evaluating the evolution of next-generation SO2 gas meters.
| Sensing Technology | Measurement Range | Key Strengths | Ideal Industrial Applications |
|---|---|---|---|
| Electrochemical (EC) | 0 - 20 PPM / 0 - 100 PPM | High selectivity, low power consumption, linear output, cost-effective OEM integration | Personal portable meters, plant perimeter safety monitoring, winery cellar entry checks |
| UV Fluorescence | 0 - 500 PPB / 0 - 10 PPM | Ultra-high sensitivity (sub-ppm), zero cross-sensitivity to H2S/CO, non-consumable optic module | Environmental air quality monitoring stations, research laboratories, trace stack gas analysis |
| Non-Dispersive Infrared (NDIR) | 0 - 5000 PPM / 0 - 5% VOL | Handles high gas concentrations without sensor poisoning, long lifespan (>7 years), immune to silicones | Raw flue gas desulfurization inlet analysis, heavy chemical synthesis process control |
The future of industrial gas monitoring lies in self-calibrating micro-sensors, AI-driven zero-drift algorithms, and optical MEMS technology. Shield Technology's R&D facility in Chengdu is currently deploying smart edge-computing algorithms that predict sensor cell degradation, notifying plant engineers months before replacement is necessary to ensure continuous zero-downtime protection.
From enclosure tooling and PCB design to custom firmware, private label printing, and specialized gas calibration.
Complete freedom over enclosure materials (die-cast aluminum alloy, polycarbonate, stainless steel), IP protection ratings (IP65/IP66/IP67), customized mounting brackets, and brand color schemes.
Tailor alarm thresholds, TWA/STEL calculation logic, Modbus registers, relay delay parameters, and multilingual display menus (English, Spanish, French, German, Arabic, Russian) directly in firmware.
Every batch produced at our Chengdu manufacturing hub undergoes automated multi-point standard gas calibration, high/low temperature aging chamber tests, explosion-proof pressure testing, and vibration testing prior to shipping.
Shield Technology provides end-to-end technical documentation and certification alignment for international distributors.
Our products meet global regulatory directives: China Compulsory Certification (3C), ATEX directive (2014/34/EU) for explosive atmospheres, IECEx international safety standards, CE compliance, and RoHS environmental standards. We assist OEM partners in acquiring local regional certifications (UL, CSA, EAC) through provided factory laboratory test reports.
We empower global distributors with dedicated technical account managers, 3D CAD step files, localized product user manuals, spare sensor replacement modules, and remote engineering support for large-scale project commissioning.
Expert technical answers addressing SO2 measurement, OEM customization, calibration, and safety linkage architecture.
Factory-direct combustible gas detectors, point-type alarms, and commercial protection devices from Sichuan Shield Technology Co., Ltd.


