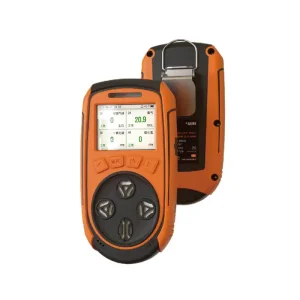
Explore our factory-direct OEM/ODM certified gas detectors, stationary controllers, and automated safety shut-off systems engineered for demanding industrial environments.
Sulfur dioxide ($SO_2$) is a colorless, toxic, highly reactive gas with a pungent, irritating odor that presents severe operational risks across global industrial facilities. As a major byproduct of fossil fuel combustion, non-ferrous metal smelting, and chemical synthesis, unmonitored $SO_2$ releases jeopardize plant safety, ruin capital equipment via acid mist formation, and cause life-threatening respiratory casualties.
$SO_2$ reacts with mucosal moisture to form sulfurous acid ($H_2SO_3$). Occupational standards dictate extremely strict thresholds: OSHA PEL is 5 ppm, ACGIH TLV STEL is 0.2 ppm, and NIOSH sets IDLH (Immediately Dangerous to Life or Health) at 100 ppm. Real-time sub-ppm tracking is critical for workforce safety.
When combined with atmospheric water vapor, $SO_2$ oxidizes into sulfuric acid mist ($H_2SO_4$). This leads to catastrophic stress corrosion cracking (SCC) in steel structures, turbine blades, and electrical enclosures. Rapid detection isolates leaks before equipment integrity degrades.
In Flue Gas Desulfurization (FGD) processes and Claus sulfur recovery units, continuous $SO_2$ monitoring ensures scrubbing efficiency, optimizes reagent dosing (limestone/ammonia), and prevents environmental non-compliance fines imposed by regulatory agencies.
Enterprise procurement teams and EPC contractors require gas detection partners capable of meeting intricate regional frameworks including EU Directive 2010/75/EU, US EPA Clean Air Act Title V, and China GB/T standards. Our OEM/ODM platform bridges compliance gaps with tailored instrument designs.
Focuses on ultra-low ambient boundary monitoring and SIL-2 functional safety for oil refineries and chemical manufacturing facilities under NFPA 72E and ISA-92.0.01.
Mandates ATEX Zone 1 / Zone 2 certification for explosive gas atmospheres alongside stringent EN 45544 requirements for toxic gas measurement instruments.
Demands heavy-duty IP67/IP68 enclosures to withstand extreme desert heat, high humidity coastal salt spray, and massive dust loads in mining and smelting plants.
Focuses on cost-effective OEM integration for legacy pulp & paper mills and copper leaching operations with rapid local technical calibration support.
Selecting the correct sensing architecture is vital for avoiding false alarms caused by cross-sensitivity to $H_2S$, $NO_2$, or humidity fluctuations. We offer custom OEM engineering across three principal detection technologies:
| Technology | Detection Range | Key Advantages | Cross-Sensitivity Profile | Ideal OEM Target Application |
|---|---|---|---|---|
| Electrochemical (SPE) | 0 - 20 ppm up to 0 - 100 ppm | High accuracy, low power consumption, sub-ppm resolution, fast response ($T_{90} < 15s$). | Filters integrated for $H_2S$, $NO_2$, and $CO$ rejection. Sensitive to severe humidity drops. | Occupational safety, personnel wearable detectors, area perimeter protection. |
| Non-Dispersive Infrared (NDIR) | 0 - 500 ppm up to 0 - 10,000 ppm | Long lifespan (> 5 years), immune to chemical poisoning, works in oxygen-free environments. | Zero cross-sensitivity to hydrocarbons. Requires moisture compensation algorithm. | High-concentration process gas streams, stack monitoring, furnace off-gas monitoring. |
| UV Absorption / Fluorescence | 0 - 1 ppm ultra-low trace levels | Extreme specificity, zero baseline drift, immune to water vapor cross-interference. | Higher initial component cost; requires optical cleaning maintenance cycles. | Environmental perimeter fenceline networks, laboratory calibration reference standard systems. |
Our customized OEM gas detectors are deployed across demanding field environments worldwide. Here is how our engineering team solves specific application challenges:
In double-contact double-absorption (DCDA) plants, $SO_2$ gas streams exceed 8% concentrations near catalytic converters. Our OEM NDIR high-range sampling units provide automated sample dilution and heat-traced sample transport to monitor conversion efficiency without damaging sensors.
Copper, lead, and zinc roasting releases huge quantities of high-temperature $SO_2$ flue gases laden with heavy dust and metallic calcines. Our point-type explosion-proof detectors feature sinter stainless-steel flash arrestors and replaceable PTFE hydrophobic filters.
$SO_2$ is widely used as an antimicrobial agent and antioxidant in wineries and fruit cold storage facilities. Lower concentration electrochemical units (0–10 ppm) with localized buzzer relay linkage ensure worker safety while preventing over-sulfuring of products.
Kraft pulp mills utilize $SO_2$ for chlorine dioxide neutralizing and bleaching processes. High humidity and corrosive atmospheres demand our IP67 glass-filled polycarbonate or 316 stainless-steel housings with hermetically sealed sensor chambers.
Post-scrubber wet stack monitoring requires accurate low-ppm $SO_2$ measurement in water-saturated gases. Integrated heated sensor blocks prevent condensation on optical windows, maintaining continuous compliance logging.
Under IMO MARPOL Annex VI regulations, marine vessel exhaust scrubbers must prove $SO_x$ compliance. Compact OEM sensor modules seamlessly integrate into marine engine control panels via Modbus RS485 communication.
As a direct factory manufacturer based in Chengdu, China, we offer end-to-end original equipment manufacturing (OEM) and original design manufacturing (ODM) services for global gas detector brands, distributors, and engineering system integrators.
Custom mold injection for branded plastic enclosures, explosion-proof cast aluminum, or 316L stainless steel housings. Private labeling, custom color schemes, silk-screened logos, and laser-etched serial plates.
Tailored software menu languages, custom alarm thresholds (Low/High/STEL/TWA), configurable 4-20mA analog scaling, HART protocol implementation, RS485 Modbus registers, and wireless IoT protocols (LoRaWAN/NB-IoT).
Every batch undergoes automated temperature-compensated gas calibration, zero-drift environmental chamber testing (-40°C to +70°C), EMC/RFI immunity testing, and vibration testing prior to factory dispatch.
Our R&D engineering center is advancing next-generation gas detection innovations to address smart industrial IoT, zero-drift requirements, and decarbonization mandates across global markets.
Integrating microcontrollers running edge machine-learning algorithms to analyze baseline noise, ambient temperature gradients, and sensor aging curves—delivering self-calibrating instruments with extended service intervals.
Replacing liquid electrolytes with non-drying, leak-free solid polymer electrolytes (SPE) to eliminate liquid evaporation risks in hot, arid mining and desert oilfield applications.
Miniaturizing Quantum Cascade Laser (QCL) path modules for ultra-sensitive, zero-cross-interference sub-ppb $SO_2$ monitoring directly integrated into compact portable safety instruments.
Get immediate expert answers to common procurement, engineering, calibration, and integration queries regarding our SO2 gas detectors.
Explore additional factory-tested gas alarm controllers, household combustible gas detectors, emergency shutdown valves, and multi-gas detection series available for global bulk supply.
Request technical datasheets, CAD dimensional drawings, sample units, or factory-direct price quotations for your global gas safety engineering projects.