Explore our high-precision industrial gas alarm controllers, commercial combustible gas detectors, and automated emergency shut-off valves engineered for direct factory deployment and OEM customization.

In modern process industries, hazardous chemical manufacturing, and municipal utility networks, gas detection systems serve as the ultimate defense mechanism against catastrophic vapor cloud explosions, toxic exposures, and oxygen-deficient atmospheres. As global safety mandates shift from reactive mitigation to proactive, continuous hazard monitoring, the role of the central Gas Alarm Controller has evolved from a passive annunciator panel to an intelligent, real-time command node.
This whitepaper provides an exhaustive technical analysis of gas alarm controller architecture, multi-protocol communication topologies, sensor-level digital processing, and automated valve-linkage safety integrity loops. Designed for system integrators, EPC engineering contractors, distributor product directors, and global sourcing executives, this document outlines the fundamental engineering criteria for evaluating OEM/ODM manufacturing partners in China.
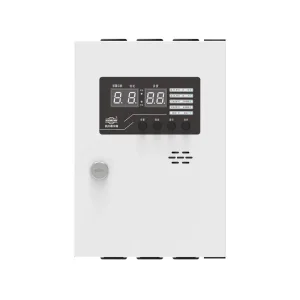
An end-to-end industrial gas safety architecture operates across three distinct operational layers: Detection, Control, and Automated Isolation. The gas alarm controller serves as the system brain, continuously ingesting field signals, evaluating concentrations against dual-stage alarm set points (%LEL, ppm, or %VOL), driving localized audio-visual alarms, and dispatching fast-acting relay commands to electromagnetic shut-off valves or exhaust ventilation networks.
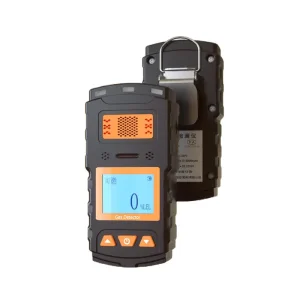
Combustible gas detectors, electrochemical toxic sensors, and IR optical units located across Zone 1 and Zone 2 hazardous areas continuously transmit gas concentrations via 4-20mA or RS485 Modbus RTU protocols.
The Gas Alarm Controller processes high-speed bus inputs, logs historical alarm events, executes voting logic (1oo2, 2oo3), and displays real-time multi-channel gas concentrations on LCD/OLED screens.
Hardwired passive relay contacts instantly trigger electromagnetic gas shut-off valves (e.g., JYFJS-011 series), isolating pipeline supply within milliseconds to prevent secondary ignition or poisoning.
To meet diverse industrial requirements ranging from compact commercial kitchens to sprawling petrochemical storage parks, Sichuan Shield Technology manufactures three main control unit architectures: Point-to-Point Analog Systems, M-Bus/RS485 Digital Bus Systems, and Hybrid Cloud IoT Intelligent Platforms.
Ideal for small-to-medium installations requiring high-density, point-to-point hardwired isolation. Each gas detector connects via dedicated 3-wire shielded cables directly to individual controller cards, guaranteeing zero signal crosstalk and single-channel fault isolation.
Engineered for large-scale industrial projects requiring long-distance transmission up to 1,200 meters. Utilizing 2-wire M-Bus or 4-wire RS485 communication, a single Shield SD8001 series controller can supervise up to 128 field detectors while drastically reducing cable installation costs.
Representing the pinnacle of Shield's technical roadmap, our next-generation controllers integrate 4G NB-IoT, Wi-Fi, or Ethernet gateway modules. System operators can monitor live gas concentrations, view historical trend charts, and receive instant SMS/App push alerts remotely.
As a direct factory manufacturer, Sichuan Shield Technology offers complete modular customization for B2B brand owners and equipment manufacturers. Sourcing partners can specify firmware algorithms, front-panel industrial styling, PCB layout parameters, and output interface configurations.
Sichuan Shield Technology Co., Ltd. operates a state-of-the-art manufacturing campus in Chengdu, China. Designated as a national high-tech enterprise and recognized as a "Specialized, Refined, Distinctive, and Innovative" enterprise, Shield combines advanced SMT automated circuit assembly with rigorous gas calibration protocols to maintain absolute quality control across large-scale manufacturing runs.
Every gas alarm controller and detector printed circuit board (PCBA) undergoes high-temperature environmental burn-in testing and automated gas calibration in zero-drift environmental chambers using certified standard gas mixtures.
Unlike trading vendors or assembly workshops, Shield designs and manufactures gas alarm controllers, point-type combustible detectors, and electromagnetic shut-off valves under one roof. This vertical integration guarantees 100% signal compatibility and eliminates supply chain delays.
Each controller unit is assigned a unique laser-etched matrix code tracking component lot numbers, SMT operator logs, inspection reports, and factory firmware versions. Standard OEM sample orders ship within 7 days, with bulk production delivered in 15–20 days.
Gas safety hazards vary significantly depending on operational environments, gas physical properties (vapor density relative to air), and regulatory mandates. Shield OEM gas alarm controllers and detectors offer adaptable configurations tailored to macro industrial and commercial applications.
Key Hazard: Methane (Natural Gas) or LPG accumulation in enclosed cooking spaces, incomplete combustion CO hazards.
System Solution: Compact SD8001 wall controller linked with SD6103K / SD6200 household or commercial detectors and JYFJS-011 aluminum alloy emergency shut-off valves. Automatically closes gas supply lines upon low-level alarm detection.
Key Hazard: Volatile Organic Compounds (VOCs), Hydrogen, Hydrogen Sulfide, and explosive hydrocarbon vapors across explosion-proof zones.
System Solution: Bus-type explosion-proof SD2100E / SD2130 point gas detectors tied via dual-redundant RS485 Modbus lines to central multi-channel gas alarm control consoles located in non-hazardous master control rooms.
Key Hazard: Underground methane buildup, carbon monoxide toxicity in valve pits, oxygen deficiency in confined spaces.
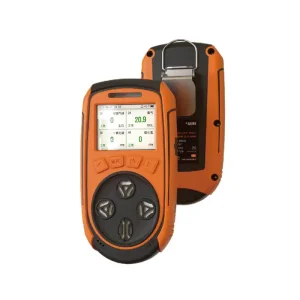
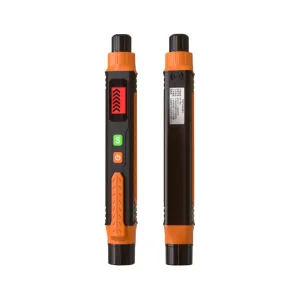
System Solution: Multi-channel gas alarm controllers integrated with 4G IoT cloud telemetry units, paired with portable 4-in-1 BTYQ-Z4 inspection detectors and stationary diffusion sensors for continuous remote supervision.
When global distributors, gas utilities, and OEM system integrators partner with Sichuan Shield Technology, they gain more than a reliable hardware manufacturer—they establish an institutional contract manufacturing partnership built upon strict Service Level Agreements (SLAs), standardized quality assurance, and long-term lifecycle support.
Our dedicated English-speaking technical sales engineers consult with your product engineering team to define exact target gas types (CH4, LPG, CO, H2S, O2, H2), operational temperature envelopes (-40°C to +70°C), local installation codes, and enclosure protection ratings (IP65 / IP67 / Ex d IIC T6 Gb).
Shield compiles custom software firmware versions supporting localized UI languages (English, Spanish, French, German, Arabic, Portuguese), customized boot logos, custom relay logic algorithms (such as delayed resetting or latching alarms), and company-specific Modbus register maps.
Working samples are manufactured and dispatched within 5 to 7 business days, complete with factory calibration certificates, circuit schematics, and test reports for client laboratory testing and local market certification filings.
Upon sample approval, mass production executes under automated ISO quality workflows. Goods are packed in export-grade protective packaging and backed by a comprehensive 24-month factory warranty, guaranteed spare parts availability for 10 years, and 24/7 engineering tech support.
Compliance with international explosion-proof and functional safety standards is non-negotiable in the life-safety industry. Shield gas alarm controllers, detectors, and solenoid shut-off valves are engineered and tested in accordance with rigorous global standards.
Fully compliant with China Compulsory Certification (CCC) standards for fire protection and life-safety gas detection equipment.
Designed to satisfy Ex d IIC T6 Gb flameproof enclosures and Ex ia IIC T4 Ga intrinsic safety protection levels for hazardous locations.
Operating under certified ISO9001 quality management, ISO14001 environmental, and ISO45001 occupational health systems.
Engineered in compliance with EN 50270 EMC requirements, UL1484 / UL2075 parameters, and SIL-2 functional safety principles.
Get definitive answers from Shield's senior application engineers regarding gas alarm controller selection, signal wiring, calibration intervals, and OEM customization.
Browse our extended portfolio of portable gas leak detectors, point-type industrial sensors, household gas alarms, and aluminum alloy electromagnetic valves available for global distribution.