Explore our factory-direct, high-precision detection units engineered for residential, commercial, and heavy-industrial safety deployments.



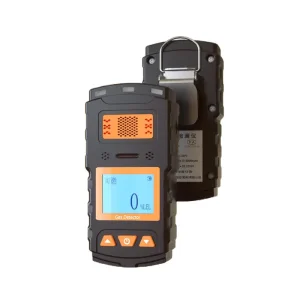
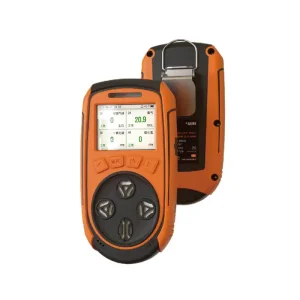

A comprehensive analysis of dual-sensing paradigms, OEM engineering requirements, and macro safety regulations shaping the gas detection market in 2025–2030.
In modern industrial and residential security infrastructure, the demand for high-reliability Carbon Monoxide (CO) Combination Detectors has experienced an unprecedented surge. Historically, property developers, industrial facility managers, and municipal gas utility engineers sourced standalone detectors for combustible gases (Methane/LPG) and toxic Carbon Monoxide separately. However, evolving building codes—such as EN 50291, UL 2034, UL 1484, and China's GB 15322—alongside the rapid digitalization of building management systems (BMS), have established dual-function combo detectors as the primary standard for proactive life safety.
Sichuan Shield Technology Co., Ltd., positioned as a premier high-tech enterprise within Chengdu's Southwest Airport Economic Development Zone, manufactures fully integrated detection-alarm-isolation systems. By synthesizing advanced electrochemical sensing for toxic CO with robust catalytic bead or non-dispersive infrared (NDIR) technology for combustible gases, Shield’s engineered combo detection units offer multi-threat intelligence within a unified hardware enclosure.
Designed for high-density residential towers and single-family kitchens, providing real-time local alarms, solenoid valve cut-off, and NB-IoT / Wi-Fi cloud alerts.
Continuous multi-point sampling in commercial heating rooms and hotel kitchens to prevent incomplete combustion hazards and explosive gas leaks.
Explosion-proof point-type detectors certified with Ex d IIC T6 ratings for harsh chemical environments, oil refineries, and pipeline hubs.
Understanding the physics, cross-sensitivity suppression, and micro-controller digital filtering in combined Methane and Carbon Monoxide safety devices.
Combustible gas leaks (such as Natural Gas / CH4 or Liquid Petroleum Gas / LPG) present a immediate explosion risk measured in Percentage of Lower Explosive Limit (%LEL). Conversely, Carbon Monoxide (CO)—a odorless, colorless byproduct of incomplete combustion—presents an extreme asphyxiation toxicity risk measured in Parts Per Million (PPM).
A truly reliable High-Quality Carbon Monoxide Combo Detector must manage two fundamentally different physical sensing principles within a single micro-chamber while preventing sensor cross-talk, humidity interference, and zero-point drift.
| Target Gas Type | Primary Sensor Technology | Typical Measurement Unit | Primary Alarm Setpoints | Physical Mechanics & Response Time |
|---|---|---|---|---|
| Carbon Monoxide (CO) | Electrochemical Micro-Cell | PPM (Parts Per Million) | 50 PPM (within 60-90 min) 100 PPM (within 10-40 min) |
Chemical oxidation of CO at target electrode generates ionic current proportional to concentration ($T_{90} < 30s$). |
| Methane ($CH_4$ / Natural Gas) | Catalytic Bead / NDIR Infrared | %LEL (Lower Explosive Limit) | Low Alarm: 8% - 10% LEL High Alarm: 20% LEL |
Catalytic oxidation raises bead temperature, altering resistance in a balanced Wheatstone Bridge circuit ($T_{90} < 10s$). |
| LPG (Propane / Butane) | Planar Semiconductor / Catalytic | %LEL (Lower Explosive Limit) | Low Alarm: 5% - 9% LEL | Gas adsorption alters surface electron depletion layer, changing conductivity ($T_{90} < 12s$). |
In real-world applications, temperature spikes, ambient humidity shifts, and domestic cooking grease can trigger severe false alarms in low-tier gas detectors. Shield solves this engineering bottleneck by integrating an ARM Cortex 32-bit MCU inside series units such as the SD6103K and SD2100A.
A gas detector is only as effective as the automated mitigation response it controls. Discover how Shield constructs cohesive safety ecosystems.
When a combo detector registers a high alarm threshold, rely-out contact terminals send an instantaneous impulse voltage (DC 9V - 12V pulse) to the connected JYFJS-011 Series Electromagnetic Shut-off Valve.
Constructed from high-tensile cast aluminum alloy or brass, the valve mechanically drops its internal plunger within < 0.5 seconds, severing the pipeline gas flow. Crucially, the valve design features a manual pull-to-reset safety mechanism, mandating human inspection and hazard clearance before gas supply can be legally or physically restored.
For multi-zone commercial structures, manufacturing complexes, and underground utility corridors, standalone alarm buzzers are insufficient. The SD8001 Series Gas Alarm Controller centralizes field detector telemetry via 4-wire M-BUS or RS-485 Modbus RTU protocol networks.
Control room operators obtain real-time digital concentration readouts (%LEL and PPM), automated event log recording, multi-stage relay output triggers for industrial exhaust fans, and direct interface with SCADA or Building Management Systems.
Strategic ODM/OEM flexibility, total cost of ownership reduction, and factory-direct quality controls designed for international importers and project contractors.
Eliminate trading intermediaries. Source directly from our Shuangliu District manufacturing hub, securing competitive unit economics for large tender tenders.
Complete branding support: custom plastic injection molding colors, laser-etched distributor logos, regional language instruction manuals, and tailored retail boxes.
Firmware pre-configuration to meet specific regional target thresholds (e.g., European EN norms, North American UL rules, or Middle Eastern municipal mandates).
100% automated chamber gas calibration using certified span gas mixtures ($CH_4, CO, N_2$), ensuring identical zero/span accuracy across multi-thousand unit shipments.
Our commitment to life-safety engineering is verified through rigorous international testing and strict manufacturing quality systems.
Sichuan Shield Technology operates an ISO 9001:2015 accredited production facility. Products across our portfolio are backed by China's mandatory CCC (3C) certification for fire-fighting safety equipment, explosion-proof dust/gas protection certificates (Ex d IIC T6 Gb), and strict EU CE directive alignment (EMC & LVD compliance).
China Compulsory Certification ensuring rigid electrical safety, flame retardancy of ABS enclosures (UL94 V-0), and strict alarm volume outputs (>85dB at 1 meter).
Heavy-duty cast aluminum enclosures certified for Zone 1 and Zone 2 hazardous areas, designed to contain internal electrical sparks without igniting surrounding gases.
In-house sensor signal amplification, dynamic noise suppression circuits, and proprietary electromagnetic valve pulse driving patents safeguard our product originality.
How Shield is shaping the future of gas monitoring through IoT integration, MEMS sensor miniaturization, and predictive AI safety analytics.
Transitioning traditional standalone alarms into cloud-linked IoT nodes that transmit real-time telemetry to municipal smart-city monitoring dashboards and mobile apps.
Adopting silicon-substrate Micro-Electro-Mechanical Systems (MEMS) sensors to reduce power consumption by up to 70%, enabling long-term battery-operated combo detectors.
Edge-computing firmware that analyzes sensor aging trajectories, automatically alerting system managers to schedule replacement calibrations before sensor exhaustion.
In-depth technical guidance from Shield's senior gas safety application engineers.
Installation height depends on the specific target gas weight relative to air. Natural Gas (Methane / CH4) is lighter than air, so a Natural Gas + CO combo detector must be mounted on the wall approximately 0.3 to 1.0 meters below the ceiling, and within 1.5 meters horizontally from the gas appliance. Conversely, for LPG (Propane / Butane), which is heavier than air, the detector should be installed 0.3 meters above the floor.
Electrochemical Carbon Monoxide sensors typically maintain accurate sensitivity for 3 to 5 years, depending on ambient exposure and temperature stability. Catalytic bead combustible gas sensors operate accurately for 3 to 5 years, while advanced NDIR infrared sensors can last up to 7 to 10 years. Shield combo units feature automated end-of-life (EOL) audio-visual warnings when sensor output drops below safe operational calibration thresholds.
Yes. Shield combo detectors and point-type alarms are engineered with multi-channel linkage terminals. For instance, the system can output a pulse DC signal to shut the JYFJS-011 solenoid valve (stopping gas supply) while simultaneously closing a passive dry contact relay (NO/COM/NC) to energize an industrial exhaust fan, quickly purging flammable or toxic vapors from the room.
%LEL (Lower Explosive Limit) represents the minimum concentration of a combustible gas in air necessary to ignite in the presence of a flame or spark (e.g., 100% LEL Methane = 5% gas by volume in air). Alarms are set at small fractions of this limit (e.g., 10% LEL). PPM (Parts Per Million) measures microscopic concentrations of toxic gases; 1% gas by volume equals 10,000 PPM. Carbon Monoxide is extremely toxic at low concentrations, requiring rapid detection at 50 PPM to 300 PPM long before explosive levels could ever be reached.
Shield provides complete manufacturing customization: custom ABS housing colors, brand logo printing, customized silk-screen labeling, regional language manuals, custom firmware alarm logic, pre-wired relay cable lengths, and custom protocol integration for smart home or industrial IoT gateways.
Complete your security infrastructure with our industrial detectors, multi-gas portable patrol monitors, and solenoid valve isolation hardware.
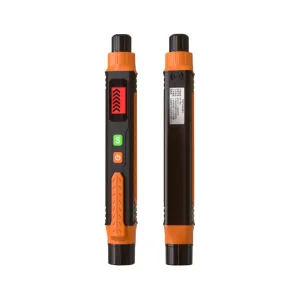

Whether you require OEM private-label household combo detectors, SIL-rated point-type industrial detectors, or complete municipal valve-linkage safety architecture, our application engineers are ready to support your project engineering specifications.
